
Logic Learning Activity Piece Tolerance: Fit, Detection and Factory Control
A buyer’s guide to matching physical answer pieces with guides, sensors and printed activities across manufacturing variation.
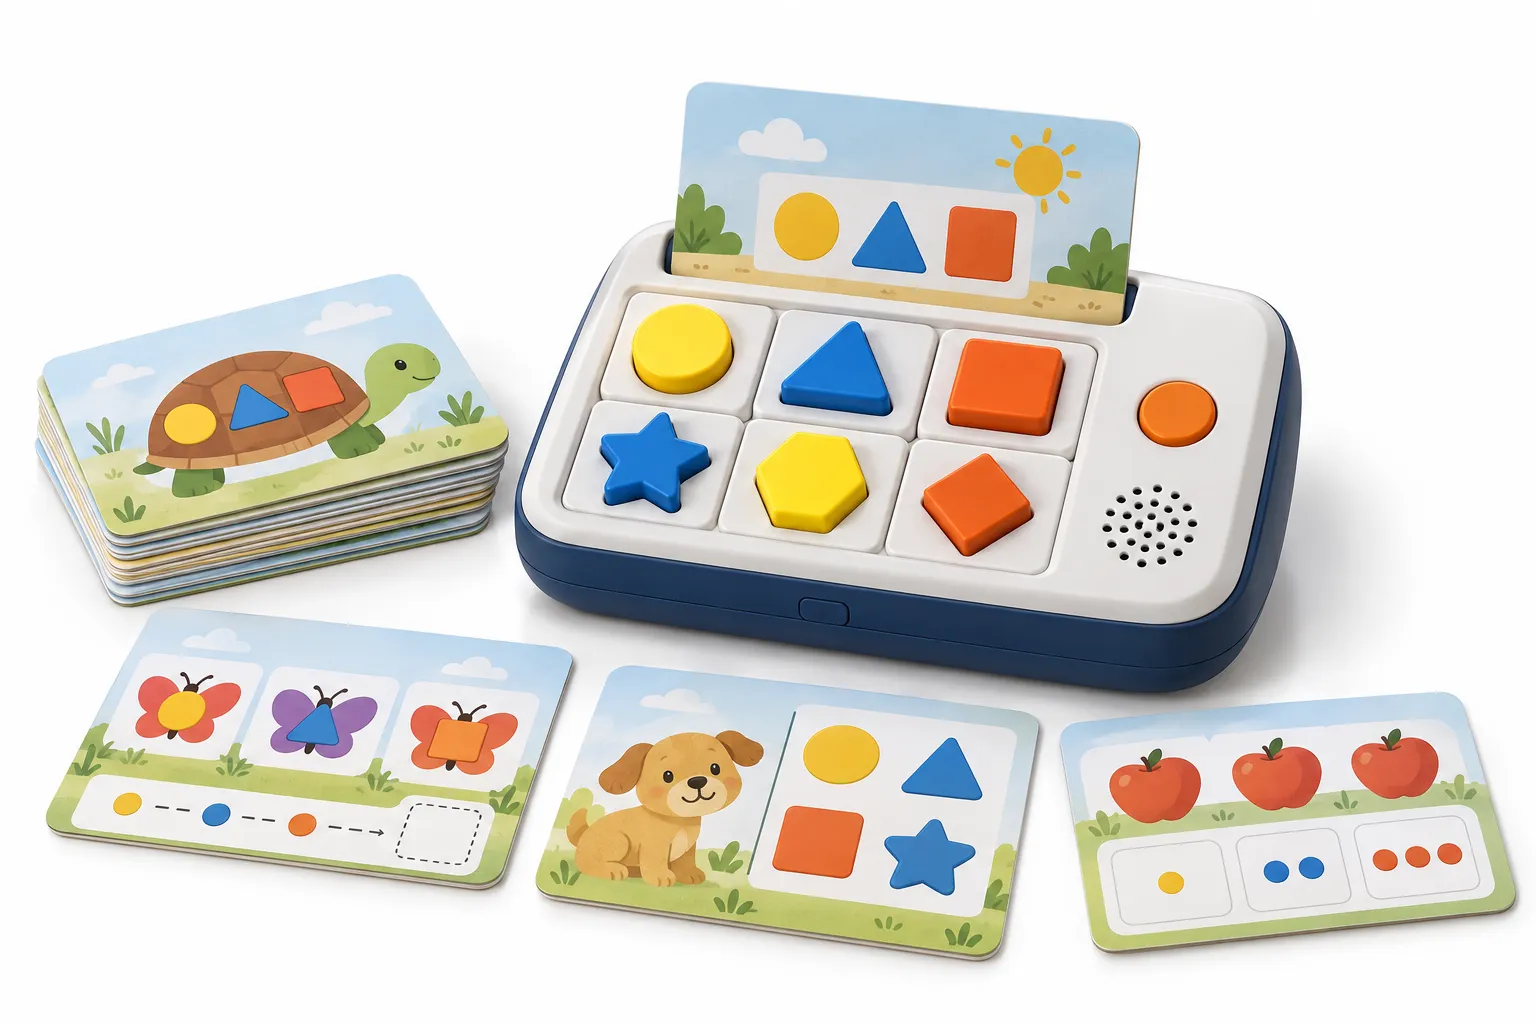
An answer piece can look correct but bind in the guide, rotate unexpectedly or sit outside the hidden detection zone. Overseas buyers often receive a confident yes and a unit price before the configuration, responsibilities and evidence are sufficiently defined. That sequence makes quotations difficult to compare and transfers unresolved decisions into samples, tooling or mass production.
This guide is written for logic toy developers, mold buyers and educational product quality teams. It answers the purchasing question behind logic learning activity piece tolerance and shows how to turn it into a comparable supplier brief, a staged approval plan and a traceable shipment decision. The objective is not to prescribe one universal solution but to expose the variables that change cost, schedule and risk.
The examples reflect normal OEM work such as customer requirements review, engineering samples, factory testing, installation preparation, print or content handoff, pilot production and shipment inspection. Numerical targets and compliance scope must still be confirmed for the actual age, market, construction and claim.
How should activity piece tolerance be specified?
Specify functional datums, critical piece dimensions, guide clearances, orientation controls, surface and edge condition, sensor target position and acceptable insertion or placement force. Allocate tolerance among piece molding, printed target, board conversion, machine guides and sensor assembly, then cross-pair worst-case pieces and machines from multiple cavities and lots.
Use the child’s action and detection margin to set functional limits; copying a nominal CAD dimension without stack analysis does not prove usability. Put the decision in the request for quotation before comparing prices. If suppliers are free to assume different materials, files, tests, accessories, packaging or delivery terms, their numbers describe different products even when the catalogue photograph looks identical.
Treat mold shrinkage making some cavities tight, piece warp changing sensor distance, decoration obscuring orientation, and guide wear increasing play as commercial as well as technical risks. Each can create a second sample round, retooling, reprinting, sorting, air freight, listing delay or customer return. A useful sourcing decision makes the risk visible and assigns evidence before money or schedule is committed.
1. Establish one RFQ baseline before contacting suppliers
Define piece shape, age group, grasping, orientation, material and shrinkage, cavities, printed decoration, guide or recess, sensor type, board datum, force and wear. Describe the finished retail or classroom set, not only the main device. Include printed content, audio or firmware, batteries and cables, accessories, instructions, packaging, languages, labels and the target market. State what is supplied by the buyer and what the factory must create.
Separate launch requirements, negotiable preferences and future roadmap ideas. Ask suppliers to identify assumptions and exclusions against the same list. An unanswered point should remain an open decision with an owner and target date; it should not quietly become the cheapest factory interpretation.
Give quotation quantities by SKU, destination, desired Incoterm, sample timing and target shipment window. Indicate whether the quantity is a market test, normal reorder or peak-season launch. This context affects tooling, material commitments, production allocation, inspection and payment terms.
2. Compare options by trade-off, not by headline feature
Molded piece dimensions and warp interact with decoration, guide geometry, activity-board registration, sensor target, firmware zone and user placement behavior. The lowest initial cost may shift work or exposure to the buyer. Conversely, the most customized option may add cost and schedule without improving the customer requirement. Use the decisions below to compare what changes in ownership, validation, repeatability and future flexibility.
Ask each supplier to label what is standard, configurable and newly engineered. A standard platform can reduce development risk only when its tested configuration is relevant to the new content, package and market. A new cosmetic shape can still alter audio, sensors, battery access, durability and tooling maintenance.
Piece geometry and handling
Balance easy grasping, orientation cues and stable placement without creating fragile projections or ambiguous fits.
For this option, define the approval condition as “Functional datums and critical dimensions identified.” Ask for piece and guide datum drawing before accepting the claim, and explicitly challenge mold shrinkage making some cavities tight during the sample review.
Tolerance and sensor budget
Divide allowable error among the molded piece, guide, printed board and sensor instead of assigning the full margin to each supplier.
For this option, define the approval condition as “Piece-to-guide clearance and force range approved.” Ask for cavity dimension and force report before accepting the claim, and explicitly challenge piece warp changing sensor distance during the sample review.
Interchangeability across production
Use pieces and machines from different cavities, dates and lots to prove that sets remain interchangeable.
For this option, define the approval condition as “Orientation and misuse behavior reviewed.” Ask for sensor-target tolerance analysis before accepting the claim, and explicitly challenge decoration obscuring orientation during the sample review.
3. Compare total quotation scope and landed consequences
A sourcing comparison should separate product unit cost from non-recurring engineering, tooling, fixtures, samples, artwork or content work, laboratory testing, inspection, packaging, inland logistics, export handling and freight. Clarify taxes, duties and destination services with qualified logistics and customs providers instead of assuming that a convenient shipping label covers every responsibility.
Ask for cavity-level measurements and a tolerance-stack explanation connected to actual sensor margin, not only overall piece dimensions. Request the same breakdown and validity period from every bidder. Confirm currency, quantity tier, scrap or overrun policy, payment milestones, tooling ownership, included sample rounds and what events reopen the price.
Model at least the first order and one realistic reorder. The first order may carry development and tooling; the reorder exposes component stability, file ownership, minimum material buys and whether the price depended on a temporary subsidy or shared stock.
| Cost or decision area | Confirm before award | Typical hidden exposure |
|---|---|---|
| Piece tooling | Cavities, tolerance and material | Uneven fit or rework |
| Detection | Target, board and sensor margin | Missed or false answers |
| Replacement | Interchangeability and version control | Installed-base mismatch |
4. Evaluate supplier evidence and execution ownership
A supplier audit should follow the proposed product route. Identify who controls electronics, molding, printing, audio or content, assembly, testing and packing. When critical work is subcontracted, document technical handoff, incoming verification and change notification rather than assuming one sales contact controls every process.
Ask for recent, product-relevant evidence with sensitive customer information removed: process flow, work instructions, fixture concept, yield summary, traceability example and corrective-action record. A generic certificate may indicate a management system, but it does not prove the requested configuration or available capacity.
Communication quality is part of supplier capability. Strong teams identify uncertainty, record revisions and explain how they will verify an answer. Repeated promises without versioned samples or evidence are a schedule warning even when the quoted price is attractive.
| Approval requirement | Evidence requested | Failure mode addressed |
|---|---|---|
| Functional datums and critical dimensions identified | piece and guide datum drawing | mold shrinkage making some cavities tight |
| Piece-to-guide clearance and force range approved | cavity dimension and force report | piece warp changing sensor distance |
| Orientation and misuse behavior reviewed | sensor-target tolerance analysis | decoration obscuring orientation |
| Sensor target remains within detection margin | cross-pair fit and detection matrix | guide wear increasing play |
| Cavity and lot variation cross-paired | wear and abuse test record | printed target offset from recess |
| Fit and detection remain acceptable after wear | replacement-piece compatibility register | replacement pieces not matching older machines |
5. Use sample gates that answer the expensive questions first
Measure and mark pieces by cavity, then cross-test high and low dimensional samples in several machines and boards. Include decorated, aged and worn units. An engineering sample may use temporary color or packaging if it is intended to resolve architecture, fit, sensing, power, audio or content risk. Mark every temporary element and simulated function so the buyer does not approve a presentation sample as though it were production-ready.
The integrated sample should use production-intent critical components, files, printed materials, firmware and set contents. Review it against a dated checklist and record exact symptoms, not comments such as improve quality. Each correction should name the affected revision and the checks that must be repeated.
Record placement force, resting position, detection result and adjacent-zone false triggers under normal and off-angle use. The approval plan should include Measure critical piece and guide dimensions, Record placement and removal force, Test orientation and predictable misuse, and Verify sensor response at tolerance boundaries. Record sample quantity, starting condition, equipment or reference media, repetitions and acceptance result. When testing reveals a failure, preserve the unit and context for investigation instead of replacing it silently.
Freeze the golden sample only after the buildable configuration is understood. Its record should identify model, hardware, software or content release, artwork, accessories, packaging and approved deviations. A physical sample cannot by itself reveal every internal component or digital file.
- Measure critical piece and guide dimensions
- Record placement and removal force
- Test orientation and predictable misuse
- Verify sensor response at tolerance boundaries
- Cycle placement and inspect wear
- Cross-pair cavities, boards and machine lots
6. Carry the purchased configuration into mass production
Control resin, molding setup, cavity identity, decoration, board coordinates and sensor assembly. First-off and periodic audits should use boundary reference pieces. The control plan should make resin and mold-cavity traceability, critical dimension and warp sampling, decoration and orientation check, and guide and board first-off approval visible at the appropriate operations. Incoming inspection confirms critical parts and materials; first-off approval confirms setup; in-process checks prevent continued output after drift; final tests screen completed units; shipment inspection confirms the packed lot.
Control reference files, firmware, test media and fixtures like physical components. Identify versions at the workstation and challenge fixtures with a known reference. A stable but incorrect fixture can approve the same defect throughout a complete production lot.
During pilot and early mass production, track first-pass yield, defect codes, rework and output by time. A final pass rate after repeated repair can hide an unstable process. Require root-cause action when failures repeat rather than accepting indefinite sorting as the production system.
Shipment inspection should select cartons across production periods and pallet positions. Verify product identity, critical user functions, appearance, complete accessories, correct language, tracking information and package integrity together. Release decisions should refer to the same defect classification and approved references agreed before production.
- resin and mold-cavity traceability
- critical dimension and warp sampling
- decoration and orientation check
- guide and board first-off approval
- piece-machine detection screen
- periodic cross-pair compatibility audit
7. Put responsibilities, changes and delivery assumptions in writing
The purchase agreement or order package should identify the specification, approved sample, files, price basis, delivery rule, payment milestones, inspection rights, change-notification duty, defect disposition, tooling or content ownership, confidentiality and applicable compliance responsibilities. Qualified legal, tax, customs and product-safety advisers should review matters within their scope.
Retain cavity references, drawings, detection data and approved boundary pieces. Review mold repair, resin, decoration, guide, board or sensor changes. Define what happens when a component becomes unavailable, a buyer edits content, a laboratory identifies a gap, a shipment fails inspection or the delivery date changes. Written escalation and approval routes reduce rushed decisions made through informal messages.
Do not use a supplier warranty as a replacement for product definition or inspection. A remedy after failure may not recover a missed retail season, platform listing interruption or reputational loss. Prevention, evidence and practical commercial remedies should work together.
For reorders, compare the current bill of material, suppliers, files, tooling status, test methods, labels and market assumptions with the archived release. Approve substitutions according to impact and retain the decision with the affected lot.
Shipment evidence pack
Index the purchase specification, approved configuration, component and file identities, first-off record, key production results, inspection report, traceability codes and accepted deviations. Retrieval should not depend on one employee or one email account.
Reconcile ordered, produced, rejected, reworked and shipped quantities. This supports commercial settlement, inventory accuracy and a faster response if field feedback identifies a pattern.
Reorder review
Require the supplier to declare changes before material commitment. Even a part described as equivalent can affect sound, battery life, recognition, color, chemical evidence or firmware compatibility.
Use retained samples and previous records as comparison evidence, but confirm current market rules and product claims. A past shipment approval does not automatically validate a changed product or destination.
8. Send a decision-ready request to shortlisted suppliers
Identify the dimensions that actually locate the piece and build a cross-pair matrix before final mold approval. Use a shared open-issues register with requirement, supplier response, evidence, owner and due date. Review it at quotation, sample, pilot and shipment gates. This prevents unresolved items from disappearing when sales, engineering and quality teams change participants.
Ask each shortlisted supplier the same questions and score evidence separately from presentation quality. A slower, qualified answer that identifies dependencies may be more valuable than an immediate price based on optimistic assumptions.
Before award, confirm that the commercial quotation and technical release describe the same product. Before shipment, confirm that production records and inspection identify that released configuration. This simple continuity is the foundation of reliable international sourcing.
Frequently asked questions
Should activity pieces fit tightly?
They should locate reliably without excessive force or binding. The range depends on age, action and sensor design.
Why test pieces from every cavity?
Different cavities can shrink or wear differently and may create fit or detection patterns.
Can firmware compensate for loose tolerance?
It may add detection margin, but adjacent zones, false triggers and physical usability limit software compensation.
Does decoration affect fit?
Paint, labels or print can add thickness, change friction or obscure orientation features.
How are replacement pieces controlled?
Use compatible dimensions, sensor targets, materials and version records, then validate against supported machines.
What should shipment inspection check?
Sample fit, force, orientation and detection using pieces and machines from different cartons or lots.
Conclusion
Activity pieces are functional interfaces, not decorative accessories. Datum-based tolerances and cross-pair evidence protect child usability and sensor accuracy across production.
A sound logic learning activity piece tolerance decision combines comparable scope, relevant supplier evidence, staged approval, factory testing and written shipment responsibilities. Send GlobalSmartToy your target market, quantity, product configuration, content status and launch date for a focused OEM review.
Authoritative references
Requirements change and differ by product. Use the current official source and qualified professional advice for the final project.