
Pilot Production and First Article Inspection for Electronic Educational Toys
What each control proves, what evidence to collect and why neither should be reduced to one perfect unit.
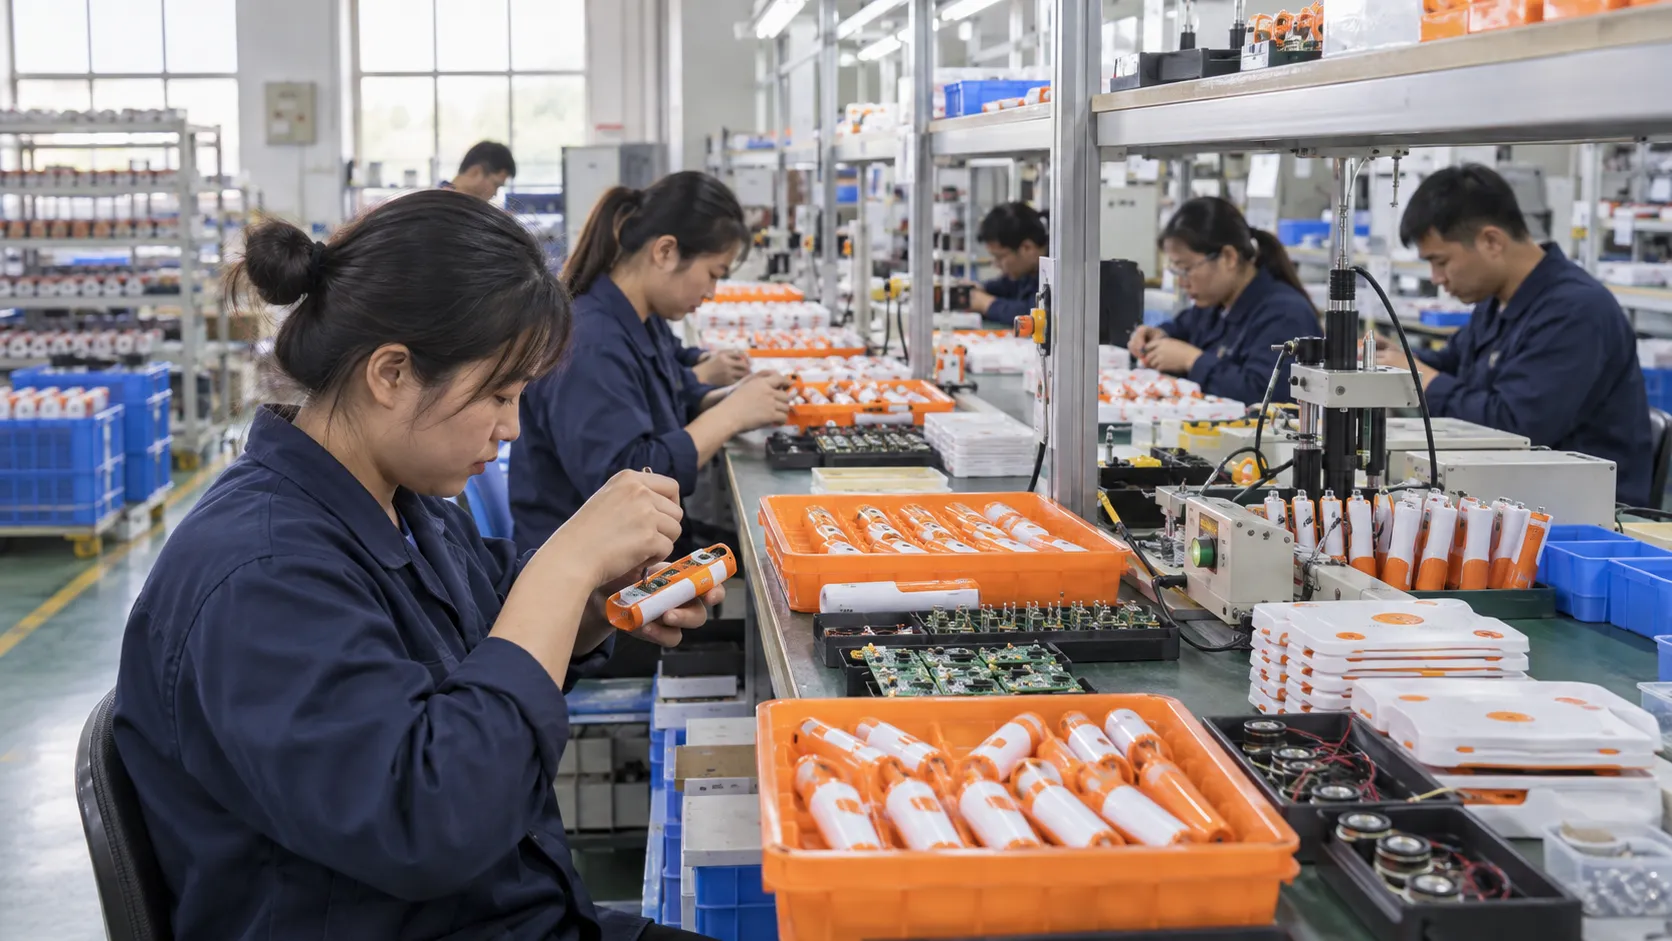
First article inspection verifies the initial production setup, while pilot production evaluates how materials, people, files and controls behave as a small manufacturing system. Buyers often discover that the visible feature is only one part of the deliverable. The commercial result also depends on how customer requirements are translated into files, components, instructions, inspection evidence and a repeatable shipment configuration.
This guide is written for buyers and quality teams releasing a new or significantly changed toy. It treats pilot production for educational toys as a practical sourcing and product-development decision. The objective is not to prescribe one universal specification; it is to show which questions should be answered, what evidence should be reviewed and where a factory handoff can fail.
Use the framework before quotation, again at sample approval and once more before pilot production. Exact limits and compliance duties depend on the model, intended age, destination market and current rules. Claims should be tied to the approved product and test conditions rather than copied from a different platform.
What should a toy pilot production run include?
A toy pilot run should use production-intent materials, suppliers, tooling, fixtures, files, operators, work instructions, tests and packaging at a quantity large enough to expose process variation. First article inspection should verify setup against the released configuration before the run continues. The pilot report should record yield, defects, cycle constraints, corrective actions and readiness decisions.
Begin by defining the use case and the decision owner. State the learner age, sales market, language, product configuration, expected interaction, order quantity and launch timing. Then identify the variables that matter most for this subject: released BOM and files, approved tooling, operator instructions, fixtures and tests, yield and defects, packaging flow. A supplier can respond accurately only when these points are visible in the brief.
Separate a desirable feature from an acceptance requirement. A feature describes intent; an acceptance requirement describes the starting condition, action, expected result and evidence. This distinction is especially important when the risks include wrong setup, mixed versions, unstable assembly, unrealistic cycle time, fixture escapes, packing errors. It enables an engineering sample to be evaluated consistently instead of by general impression.
1. Translate customer requirements into a pilot-production brief
Define pilot quantity and success criteria from risk, novelty and process complexity rather than selecting a token number. Put every open assumption in a question log and identify who will approve the answer. Reference products can clarify size or interaction, but they do not replace written requirements because their internal components, rights, reports and manufacturing history may be unknown.
Prioritize the brief as mandatory, preferred and optional. Conflicts become easier to resolve when the team knows which outcome protects the user and commercial promise. Record target values only when the measurement method is also defined. Otherwise, terms such as durable, clear, fast or premium can create different expectations for the buyer, engineer and inspector.
2. Review the complete line setup, process controls and release evidence instead of one component
The pilot should include incoming materials, programming, assembly, in-process controls, functional test and retail packing as one flow. Map the interfaces between hardware, firmware or content, printed material, enclosure, power, accessories and packaging where they apply. A change at one interface can alter another result: material thickness can affect detection, compression can affect speech clarity, or package configuration can alter transport exposure.
Ask the supplier to distinguish proven platform capability, configurable behavior and new development. The distinction affects quotation, lead time and validation depth. A familiar component does not automatically make the final configuration proven. The team should review interactions using production-intent parts and files before releasing mass materials.
| Decision layer | Question to close | Evidence to retain |
|---|---|---|
| First article | Is setup correct before continuation? | Measured inspection report |
| Pilot flow | Can the process repeat at intended method? | Yield and cycle records |
| Defects | What failed and why? | Root-cause action log |
| Release | Are open risks acceptable? | Readiness decision |
3. Build a staged sample and approval plan
Do not substitute hand-built engineering samples for line-made units when evaluating fixtures, operator instructions or cycle time. Use early samples to answer high-risk questions, not to imitate a finished retail unit before the system is stable. Label temporary parts and simulated functions. Approval should identify exactly what has passed and what remains open so a cosmetic sample is not mistaken for approval of production electronics or content.
The integrated sample should use the intended interaction files, materials and critical components. Evaluate it against a dated checklist and record failures with photos, video, measurements or file identities as appropriate. Corrections should be issued through a change list; the next sample should state which changes were incorporated and which tests were repeated.
4. Define factory testing around realistic product use
Sample units across the run and investigate recurring symptoms by station, component lot, operator and time. The core test set should cover first-off dimensions, critical functions, version identity, process yield, pack-out, corrective-action verification. Conditions need enough detail to repeat the result: unit state, power condition, content or test media, action, number of cycles and acceptance outcome. Testing only the easiest function can allow a configuration error to reach packing.
Separate development verification, line testing and shipment inspection. Development explores design limits; line testing quickly detects assembly or programming errors; shipment inspection samples the completed lot and pack-out. Each serves a different purpose. For critical configuration items, identify whether a controlled 100 percent check is required in addition to sampled inspection.
5. Control production variation and shipment identity
Close critical actions and update instructions, fixtures and control plans before ramping; segregate pilot units if their status differs. Incoming materials should be checked against approved identity and relevant performance. First-off units verify setup before volume production. In-process checks should occur where a defect can still be corrected efficiently, while final functional tests confirm that the assembled product matches the released configuration.
The shipment record should make first article report, pilot lot identity, yield data, defect log, readiness approval traceable to the finished lot. Inspect cartons from different pallet positions and production times rather than selecting convenient samples from one location. Confirm the product, language, accessories, labels and retail package together because a correctly built unit in the wrong SKU package is still a serious customer defect.
6. Compare quotations, timing and lifecycle cost on equal scope
Account for pilot material, setup, testing and possible rework in the project scope; the cost buys evidence before the full lot is exposed. Request itemized assumptions for development, tooling if any, content or prepress work, samples, testing, packaging and production. Compare quotations against the same configuration and Incoterm. A low unit price is not comparable if essential engineering or inspection work is excluded.
Plan approval time as part of the critical path. Factory working days, buyer review days, correction rounds, laboratory time, material purchasing and shipment booking should be visible. For reorders, compare the new bill of materials and release files with the archived baseline. Cost-saving substitutions require documented review because they may change performance, evidence or customer experience.
7. Use an evidence-based release decision
Use a documented go, conditional-go or hold decision with named actions rather than assuming completion of the run equals approval. A release meeting should review unresolved issues, deviations, pilot results, packaging readiness and destination-market documentation. “Looks good” is not a release criterion. Name the exact product version, accepted evidence and any action that must close before shipment.
Keep the conclusion proportionate to the data. A small sample can confirm a function under stated conditions but cannot prove unlimited life or universal market acceptance. Credible B2B communication explains the test conditions, remaining responsibilities and change triggers. That approach supports both buyer decisions and later investigation if field feedback appears.
Implementation record: applying pilot production for educational toys to a real project
Start with a controlled baseline, not an informal sample
For a production validation project, the first useful baseline combines the written requirement, approved physical sample, product configuration, content release and test evidence. Photographing a sample or calling it “approved” is not enough. Record its model, language, firmware or content identity where relevant, materials, accessories, package version and any accepted deviation. The baseline gives purchasing, engineering, the factory line and the shipment inspector the same reference when pilot production for educational toys decisions move from discussion into production.
Run a short cross-functional review before freezing that baseline. The buyer should confirm customer requirements and target market; engineering should identify technical constraints and dependencies; quality should convert critical promises into observable checks; and production should confirm that the proposed method can be repeated at line speed. Open points need an owner and due date. If an assumption cannot yet be verified, label it as provisional instead of allowing it to appear as an approved fact in the quotation or instruction.
Use pilot evidence to expose variation and handoff errors
A pilot is most valuable when it reproduces the intended materials, tools, files, operators, inspection steps and packing flow. Select units from the beginning, middle and end of the run, then test normal use and the difficult conditions identified in the risk review. Record individual results rather than only writing “pass.” For electronic learning products, useful evidence may include version identity, response behavior, audio clarity, power state, repeated interaction and pack-out accuracy, depending on the subject of the article.
Review failures by mechanism and process stage. A symptom found during factory testing can originate in an incoming component, file release, assembly method, fixture, work instruction or inspection rule. Correcting only the failed unit does not demonstrate control. The team should document containment, determine the likely cause, update the source process and rerun a defined verification sample. When evidence is mixed, keep the conclusion narrow and collect more data rather than making a confident but unsupported claim.
Carry the approved decision through shipment and repeat orders
Before shipment inspection, translate the approval package into a concise inspection plan. It should identify critical functions, sample selection, test media or fixtures, cosmetic limits, packaging checks, version verification and the records that must accompany the lot. Random sampling can indicate lot quality, but it does not replace process controls for safety-critical or configuration-critical characteristics. Define any 100 percent checks separately and confirm that their fixtures and pass criteria are controlled.
For reorders, begin from the archived release rather than from a fresh verbal description. Compare the bill of materials, approved suppliers, files, firmware, artwork, labels, test methods and regulatory assumptions. Any proposed substitution should state why it is needed, what characteristics may change and what revalidation is required. This disciplined comparison protects customer requirements when staff, component availability or production timing changes between orders.
Finally, use field feedback as structured input. Record model, lot, market, usage conditions and symptom; compare the report with retained samples and production records; and separate isolated damage from a repeatable pattern. The purpose is not to claim that every project is risk-free. It is to create traceable evidence showing what was specified, what was tested, what was shipped and how new information was handled. That is the practical foundation of trustworthy pilot production for educational toys guidance.
Create a buyer review worksheet before quotation
A useful review worksheet has four columns: requirement, current decision, evidence needed and responsible owner. Populate it first with the six target areas that commonly change a children’s electronic product: user and age, interaction, content and language, hardware and power, package configuration, and destination market. Add the subject-specific decisions from this guide. For each row, state whether the item is approved, open, supplier-proposed or outside the current scope. This prevents an unanswered question from silently becoming a factory assumption and makes different quotations easier to compare.
Use the worksheet during the sample meeting rather than relying on comments scattered across email and chat. Link each decision to a dated file, marked photograph, measured result or physical reference. When the buyer accepts a deviation, record what differs, why it is acceptable and whether labeling, instructions, testing or price changes. Before issuing the purchase order, reconcile the worksheet with the quotation, approved sample and pack-out list. The result should identify one buildable configuration, not a collection of individually approved materials that were never reviewed together.
Add a final column for change triggers. Examples include a different component supplier, edited audio, new language, revised printed content, new package claim, destination-market change or a manufacturing-site move. For every trigger, identify who reviews the impact and which sample, document or test may need to be repeated. This turns the worksheet into a lifecycle control rather than a one-time RFQ form. It also gives customer service and reorder teams a faster route back to the evidence behind the released product. Record the decision date and effective production lot so warehouse stock, shipment inspection and later complaints can be compared with the correct configuration across changing commercial production conditions.
Frequently asked questions
When should pilot production for educational toys be discussed with a supplier?
Discuss it before quotation so the supplier can identify platform limits, custom work and evidence needs. Reconfirm it at integrated sample approval, pilot production and any later change.
Is a pre-production sample the same as a pilot run?
No. One sample can verify configuration, while a pilot run exposes process variation and handoffs across multiple units.
Can pilot units be sold?
Only if they fully meet the released product and compliance requirements and their status is approved. Do not assume pilot automatically means saleable.
What if the pilot yield is low?
Contain affected units, analyze mechanisms, correct the process and verify improvement before scaling. Rework alone does not prove readiness.
What should shipment inspection verify for this subject?
Verify the released configuration, representative critical functions, correct files or versions where relevant, appearance, accessories, labels and packaging. The exact sampling and any 100 percent checks should be agreed before production.
How should a repeat order be controlled?
Start from the archived golden sample and release package. Compare components, suppliers, files, process, tests and market assumptions, then approve and revalidate any change before mass production.
Conclusion
Pilot production provides confidence only when it challenges the intended process and produces traceable learning. The reliable route is to define observable requirements, examine system interfaces and connect sample approval to production evidence. That turns a broad buying question into a controlled decision.
GlobalSmartToy recommends confirming the exact configuration and destination-market responsibilities in writing before commercial release. Share the product concept, target users, languages, quantity and timing to begin a focused technical review rather than a generic quotation.
Authoritative references
Requirements change and differ by product. Use the current official source and qualified professional advice for the final project.