
Toy Material and Printing Chemical Compliance: A Buyer’s Control Plan
How to connect the bill of materials, supplier declarations, risk-based testing and factory change control for educational toys.
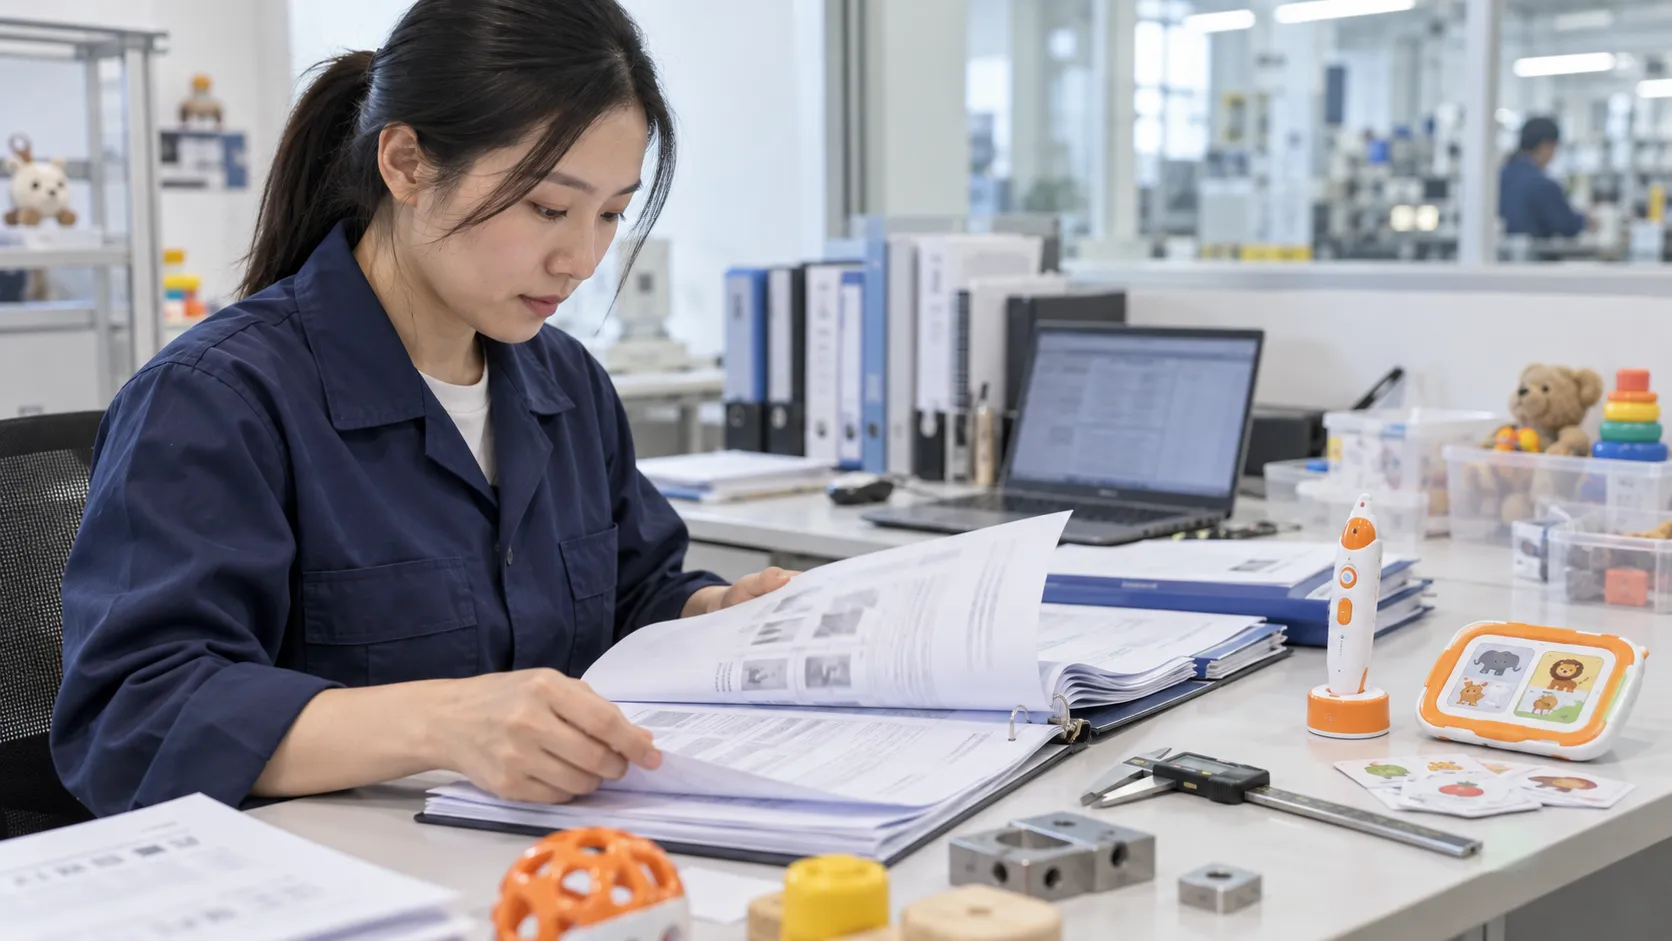
Educational toys combine plastics, paints, inks, coatings, adhesives, paper, board, electronic components, cables and packaging. A talking pen set can contain more material variations in the books and accessories than in the device. Chemical compliance must therefore follow the exact bill of materials and production suppliers, not a product name or visual similarity.
US and EU requirements use different legal frameworks and substance scopes. The US may involve CPSIA lead and phthalate requirements and ASTM F963 provisions for applicable toys. The EU toy-safety framework, REACH and other legislation can be relevant depending on material and product. Qualified laboratories should determine the actual test plan.
This guide explains supplier evidence, sample selection and change control. It does not provide universal limits or claim that declarations replace testing. Use current official sources and professional compliance advice for the destination market.
How should toy material chemical compliance be controlled?
Toy material chemical compliance should be controlled through an accessible-material and BOM inventory, approved suppliers and specifications, current declarations or reports linked to exact parts, risk-based laboratory testing of representative production materials, traceable color and coating variants, incoming verification, and formal review before any plastic, pigment, ink, adhesive, battery or print supplier changes.
Start by identifying what children can touch, mouth or access during intended and foreseeable use, including after appropriate use-and-abuse tests. Hidden electronics and inaccessible adhesives may have a different exposure analysis from painted buttons or book coatings. Qualified reviewers should make the final determination.
Break compound parts into materials and finishes. A plastic button with pad printing is not one chemical item. The substrate, pigment, ink and protective coating may come from different suppliers and carry different evidence. Record color because pigment can change substance risk.
Use evidence in layers. Supplier declarations and specifications support material control; laboratory testing supports conformity evidence; incoming and change controls support continued production. No single document performs all three roles.
1. Create an accessible-material inventory
List every part, material, color, finish, supplier and accessibility. Include housing, buttons, printed graphics, soft components, cords, cables, battery contacts, books, cards, stickers and packaging items that form part of the toy. Link each entry to drawing and BOM numbers.
For printed content, separate paper or board, ink systems, lamination, varnish, adhesive, binding materials and foil or special finishes. A printer's general compliance statement may not identify the exact combination used for the order.
Photographs and exploded diagrams help laboratories select samples and help purchasing recognize changes. Update the inventory when artwork adds a new ink, a card finish changes or an accessory is introduced.
2. Map market requirements to materials and exposure
Use official US CPSC and EU sources plus qualified laboratory advice to identify applicable chemical requirements. Age, product type, material, accessibility and market influence the plan. Avoid copying a generic list of tests from an unrelated toy.
In the United States, applicable children's-product requirements can include limits on lead in accessible substrate materials, lead in paint or surface coatings, and specified phthalates in accessible plasticized components, along with relevant ASTM F963 provisions. Confirm current rules and exemptions.
For the EU, toy-safety chemical requirements and REACH restrictions may both be relevant. Regulation (EU) 2025/2509 introduces future changes under its transition, while the current route remains important in 2026. Ask the laboratory to document the legal and standard basis for its test plan.
3. Qualify material, coating and printing suppliers
Purchase to written specifications that identify grade, color, coating system and approved manufacturer. Review supplier quality history and change notification. A reseller's part name without original-material identity can weaken traceability.
Request evidence linked to the exact item and current formulation. Check issuer, model, color, date, test scope and laboratory. A declaration for white resin may not cover every pigment; a report for one ink system may not cover foil or varnish added later.
For printers, approve substrate and finish construction as well as artwork. Confirm how inks, adhesives and laminates are controlled, how excess material is stored and how substitutions are prevented during peak production.
| Material layer | Record to identify | Common gap |
|---|---|---|
| Plastic and pigment | Resin grade, color masterbatch and supplier | Only finished color name recorded |
| Paint or ink | System, color and application | Generic supplier declaration with no SKU |
| Printed board | Substrate, ink, finish and adhesive | Paper report excludes coating or glue |
| Cable or soft part | Polymer, color and formulation | Visually similar substitute used |
4. Select representative samples and testing strategy
Provide the laboratory with the complete material inventory, colors, variants, age and construction. Let qualified experts determine component grouping, composite testing where allowed, worst-case selection and sample quantity. Undisclosed variants can make a report incomplete.
Use production-intent materials from identified suppliers. Engineering samples painted by a model shop may not represent mass production. Record lot and source of submitted components. Review report photographs and descriptions against the actual BOM.
Testing frequency and periodic programs depend on market rules, material control and responsible-party policy. A risk-based plan may use supplier evidence and verification, but should not assume an old report remains valid after formulation, supplier or process change.
5. Verify materials before and during production
Incoming inspection should confirm part identity, supplier, lot, appearance and required documentation. More advanced verification may be used according to risk. Keep unapproved or pending materials physically and electronically separated from released stock.
Production should use the released BOM and process. Control paint mix, ink, adhesive, curing and regrind where relevant. Record lots for critical materials and finished production so a later question can identify affected shipments.
Do not allow line-side substitution because a color looks close or a supplier says it is equivalent. Route shortages through formal change control, technical review and any required compliance verification.
6. Control books, cards and decorated surfaces
Printed learning components are part of the toy set and may be handled repeatedly. Confirm substrate, ink, lamination, varnish, adhesive and binding. Consider foreseeable mouthing for younger ages and any cleaning claims. The finished construction, not only base paper, needs review.
Pad printing, screen printing, heat transfer and labels on the device should use approved systems and adhesion appropriate to use. If decoration wears, it can affect appearance and potentially exposure. Include durability and appropriate chemical review in the plan.
Keep print suppliers on the approved list and preserve press or batch information as appropriate. Artwork changes that add colors or finishes should trigger material review before the print run.
7. Maintain evidence through changes and reorders
Create a compliance-impact field in engineering change requests. Identify affected materials, colors, suppliers, reports, declarations and markets. Obtain laboratory or responsible-party decisions before purchasing volume material.
At reorder, compare the current BOM and supplier list with the tested release. Check report validity, standard updates and new legal requirements. Long-running products are vulnerable to silent supplier drift when documentation is reviewed only at first launch.
Shipment records should connect finished lot with relevant materials and artwork versions. Final inspection cannot identify every chemical formulation, so prevention, purchasing control and traceability are essential.
Build a material data system that follows the real bill of materials
Identify every material and supplier layer
Create a material declaration table covering molded resins, masterbatch, paint, ink, coating, adhesive, metal, wire, PCB, battery, speaker, paper, board, lamination, textile and packaging items as applicable. Record supplier, grade, color, use location and approved evidence. Generic descriptions such as ABS or eco ink are not enough to distinguish formulations or production sources.
For printed learning products, include substrates and post-print processes. The same visible color can use different ink systems, and a film or varnish may introduce another material. Map each material to the part or page where it is used, especially where child contact, wear or foreseeable mouthing affects the risk assessment.
Use risk-based evidence and sample selection
Work with qualified compliance specialists to determine applicable chemical requirements and test strategy for target markets. Consider material type, color, coating, accessibility, supplier history and existing valid evidence. Composite or grouped testing may be possible in some circumstances, but it can make root-cause identification difficult; the laboratory and responsible business should agree the approach.
Test samples must represent production materials and colors. Record lot, supplier, product revision and sampling date. Review laboratory reports for model and material identity, methods, limits, results and accreditation scope rather than accepting the word pass. Resolve any ambiguity before relying on the report for certification or market documentation.
Control changes after approval
Purchasing specifications should name approved grades and suppliers and define prohibited substitution. Incoming controls can include identity documents, color, labeling, batch and selected physical checks. Higher-risk coatings and inks may require additional lot evidence or periodic verification. Store materials to prevent mix-up and use traceable issue records on the production line.
A change request should state what changes, why, affected models and evidence proposed. Compliance, engineering and quality owners decide revalidation before use. Link finished-goods lots to relevant material lots. This traceability does not prevent every problem, but it makes containment and investigation far more precise than asking which red paint was used months later.
For reorders after a long gap, reconfirm supplier, grade and formulation status rather than assuming the old purchasing code still represents the same material. Request notice of discontinuation or formulation change from critical suppliers where possible. Review retained samples for color and finish, but do not use appearance alone as proof of chemical equivalence.
Keep declarations and reports in a searchable index with product, part, material, color, supplier, standard, date and expiry or review status. A structured index helps teams find gaps before a customer audit and prevents an unrelated report from being attached simply because the material name looks similar.
Frequently asked questions
Does a material declaration replace toy testing?
No. Declarations support supplier control, while applicable testing and conformity decisions require product-specific evidence. Use both within a risk-based compliance program.
Can one plastic test cover every color?
Possibly only when qualified reviewers support grouping based on formulation and risk. Pigments and additives can differ, so disclose every color to the laboratory.
Are printed books part of toy chemical compliance?
When sold as part of the toy set, their paper, inks, coatings, adhesives and construction should be included in the product review according to accessibility and market requirements.
What happens when a paint supplier changes?
Pause use, review the new formulation and evidence, and obtain qualified decisions on testing or documentation before production approval.
Does REACH replace toy-safety chemical requirements?
No. Multiple EU legal requirements may apply. The responsible economic operator should identify the complete current framework for the product.
Can final inspection detect chemical noncompliance?
Ordinary visual shipment inspection cannot verify chemical formulation. Compliance depends on approved materials, supplier controls, laboratory evidence, change management and traceability.
Conclusion
Toy chemical compliance begins with a detailed material inventory and ends with production that still uses those approved materials. Plastics, pigments, coatings, printed content and adhesives need traceable specifications and suppliers.
Combine current official requirements, qualified laboratory planning, representative testing, incoming controls and disciplined change review. That is more reliable than collecting generic reports after the product is already packed.
Authoritative references
Requirements change and differ by product. Use the current official source and qualified professional advice for the final project.